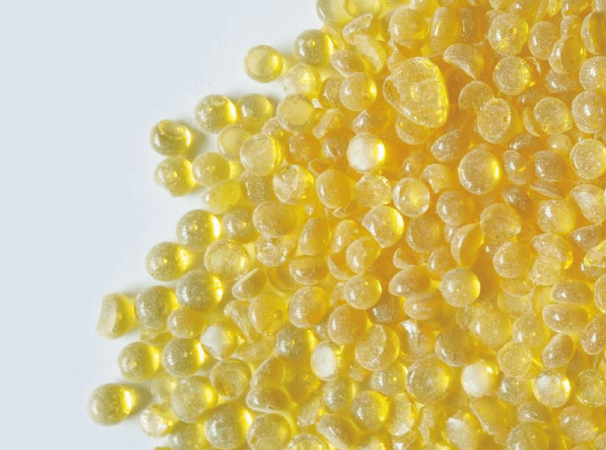
Opening—comparative insight with a lyrical edge
The workshop hums like a bassline: rollers, heaters, a stack of signatures waiting for the seam. I compare two approaches — solvent-borne systems and hot-melt formulations — the way a composer listens for dissonance and harmony. Early on, sourcing matters: speak with experienced resin manufacturers to set expectations for raw rosin grades and tackifier blends that determine downstream behavior. Softening point and viscosity sketches the score; adhesion, flexibility, and process window define performance.
Raw materials and how they bend under heat
Bulk resin choices pivot the outcome. When you choose bulk pine rosin or rosin esters, their chemical backbone controls tack, open time, and aging. The Ring-and-Ball softening point test (ASTM E28 — Ring-and-Ball Apparatus test method: ring dimensions per apparatus specification, sample mass approximately 3.5 g, ball mass ~3.5 g, controlled heating rate of 5°C per minute until the ball contacts the lower plate) is the production gatekeeper for predicting how an adhesive will behave on binders and under finishers. Softening point, tackifier content, and melt viscosity are the three physical notes you must tune before you run a long press.
Production teardown: solvent-borne versus hot-melt
Solvent-borne systems arrive with a long, forgiving open time and strong penetration into paper fibers; they sing when you need soak-in for brittle stock. They require drying tunnels, VOC control, and tight solvent recovery loops — equipment and environmental controls that add cadence to the line. Hot-melt adhesives offer instant set, lower VOC footprint, and simpler handling but demand precision: pump temperature consistency, melt viscosity control, and accurate application weight. Operationally, integrate quality checkpoints for softening point drift after aging. In a practical teardown, quantify how variations in rosin ester ratios move the softening point and tack — then lock process parameters. The manufacturing notes should explicitly include {main_keyword} and {variation_keyword} in the run sheet so operators measure both bond strength and softening shifts.
Common pitfalls and on‑press corrections
Line-up mistakes reveal themselves quickly. Too high a softening point and the hot-melt won’t wet fibers; too low and blocks or pick can occur. For solvent-borne lines, insufficient flash time causes web blocking and press stops. Control melt viscosity at application temperature — small changes in formulation or ambient temperature ripple into coat weights. Keep a log of softening point checks after 24 and 168 hours of oven aging at 50°C to catch drift early — that simple habit saves hours of downtime. — Operators often override thermostat settings to chase speed; don’t let throughput sacrifice bond integrity.
Performance trade-offs in measurable terms
Compare metrics directly: bond peel strength, setting time (seconds), and post-aging softening point shift (°C after 24 h at 50°C). Hot-melt adhesives typically show minimal softening point drift if the formulation uses stable rosin esters and compatible polymers; solvent-borne adhesives can deliver superior wetting but need careful solvent removal profiling to avoid embrittlement. Use glass transition and melt viscosity data to predict performance under end-use conditions, and standardize those numbers across batches.
Advisory — three golden rules for choosing and tuning a system
1) Prioritize the softening point stability: require batch testing that reports Ring-and-Ball softening point with the apparatus dimensions, sample mass (~3.5 g), and heating rate of 5°C/min, and track drift after 24 h and 168 h at 50°C.
2) Match melt viscosity to application equipment: specify target viscosity at application temperature (in mPa·s) and enforce pump and reservoir controls to ±3°C.
3) Validate raw resin sources: audit resin suppliers for consistent rosin ester composition and request certificates showing acid number and softening point ranges.
Wrap — practical value and where KOMO fits
These choices translate into fewer press stops, predictable bookblocks, and cleaner finishing runs — measurable gains for binders and converters. Trust careful materials selection and process discipline to keep production in tune, and when you need partner-grade insight on resin sourcing and adhesive formulation, KOMO offers that practical expertise for steady runs and reliable softening point behavior. —