



Introduction
I once watched a line operator beat a stubborn jam with nothing but a screwdriver and a stubborn grin—true story. In that same plant, a single wet tissue machine sat idle for two hours last quarter, costing the team about 1,200 sheets an hour in lost output (that adds up fast). We’re talking machine downtime, waste, and frustrated crews. So what if small design changes could cut those hours in half? I ask that because data shows many shops lose 5–10% of daily capacity to stoppages — and I want to know how we fix that without breaking the bank. Let’s dig into why the usual fixes miss the mark and where to focus next.
Part 2 — The Hidden Flaws in Traditional Solutions
Why do tried-and-true fixes keep failing?
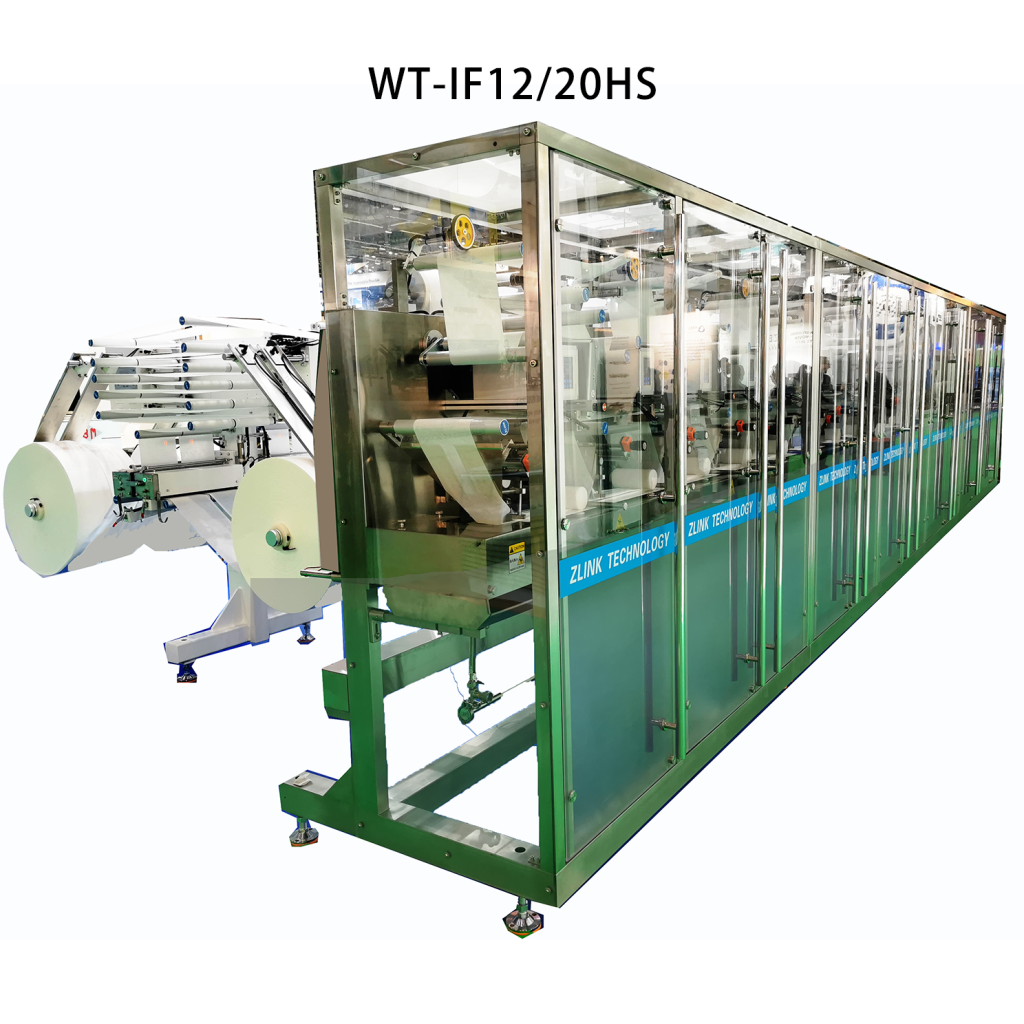
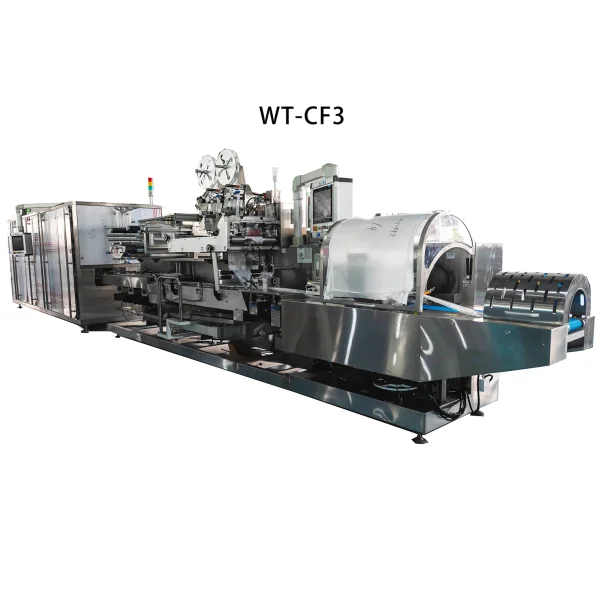
When teams reach for quick upgrades they often ignore the root causes. I’ve seen plants add sensors, then wonder why alerts keep piling up. A better starting point is a proper look at the full line, especially when you consider a customized wet wipes manufacturing machine—it’s not just a wrapper and a cutter. The PLC logic, servo motor tuning, dosing pump calibration, and embossing roller alignment all interact. If one element is off, the rest compensates—and that creates new problems. Look, it’s simpler than you think: fix one subsystem, and another shows its true limits.
Take maintenance planning. Most shops do reactive fixes. That means a jam happens, someone clears it, and the line resumes. No one records the exact cause, so patterns never emerge. I’ve recommended simple logging steps—time, error code, operator note—and the results were immediate. Teams spotted recurring faults tied to a specific embossing roller offset and corrected it. The change cut waste and made shifts less frantic. We also learned that power converters and basic human factors (how a panel is mounted or labeled) matter just as much as high-end sensors. That’s the ugly truth: high-tech is worthless without thoughtful integration.
Part 3 — Future Outlook: Practical Paths Forward
What’s Next for Operators and Lines?
I see two sensible paths. One is gradual: tune what you have—better PLC recipes, more precise servo calibration, cleaner dosing pump schedules. The other is selective upgrade—swap a few bottleneck parts or add targeted edge computing nodes to collect local data. Both routes can involve a customized wet wipes manufacturing machine approach: tailor the line to how your crew really works, not to a generic spec sheet. I prefer starting small and measurable. You don’t need to replace everything to get visible gains—funny how that works, right?
To help choose, I use three simple metrics we can all check. First: mean time between stoppages (MTBS). Track it weekly. Second: scrap rate per shift. Keep it in single digits and watch trends. Third: operator recovery time—how long it takes to clear an event and restart. Those three tell you where to act. If MTBS is low, look at mechanical alignment. If scrap spikes, check dosing and embossing. If recovery time is long, simplify controls or improve the human interface. Use these and you’ll see real change.
I’ve spent years on floors like yours. We can be pragmatic and still smart about upgrades. If you want a partner who respects operators and tech, check the way teams work with tailored lines—then test small changes, measure results, repeat. For equipment and trusted solutions I recommend taking a close look at ZLINK — they get the balance between machine bits and human habits.
