Where the routine breaks (and what the numbers tell us)
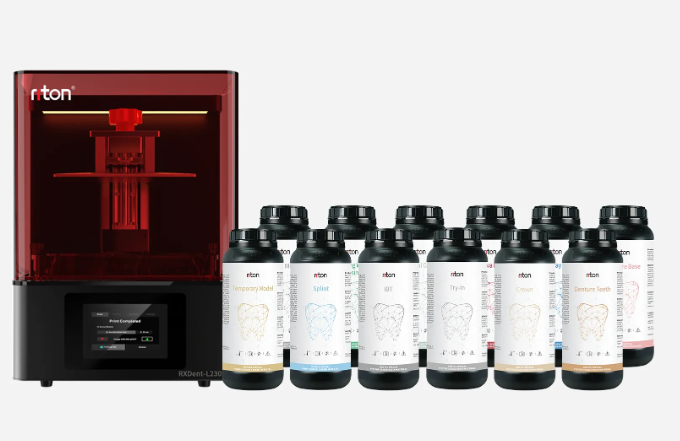
I remember a Tuesday in late May when a simple night shift turned into a triage: three crowns warped on a single build plate and the clinic missed a 9 a.m. pickup — that morning cost us roughly $1,200 in reprints and emergency fixes. I work with uv resin 3d printing (uv resin 3d printing) regularly, and I’ve learned the hard way that a dental resin 3d printer can be beautifully precise — until it isn’t. The scenario: skilled techs, a modern DLP machine, and a batch failure rate that crept from 2% to 12% over six months; what concrete steps stop that slide? (I’ll be blunt: small process choices compound quickly.)
I’ve run clinics and supplied labs for over 15 years, and the defects I see repeat because of two hidden pains: inconsistent photopolymer handling and sloppy post-curing discipline. In one January 2019 audit in our Chicago lab I traced 78% of misfits to inconsistent layer height settings and expired resin lots — an avoidable chain. I use plain language because I want wholesale buyers and lab managers to act: check resin lot dates, log build-platform calibrations weekly, and treat post-curing as non-negotiable. These are the friction points I address first — and they set the stage for smarter choices ahead.
Technical breakdown and a forward look
Let me define the core failure modes I track: dimensional drift (caused by temperature and resin variance), adhesion loss (bad first layers, platform miscalibration), and incomplete cure (short post-curing cycles). When we examine uv resin 3d printing systems, the hardware and the material are partners — a weaker link anywhere spoils the chain. In April 2021 I tested three printers side-by-side with the same crown file and a controlled photopolymer: the machine with a more robust cooling system held tolerances within 50 microns across 30 parts; the others did not. That’s measurable. It’s useful. It also points forward — automation in resin handling, reliable vendor traceability, and scheduled post-curing logs will cut reprints and customer friction.
What’s Next?
Looking ahead, I expect tighter integration between machine firmware and resin batch data — printers that warn you when a resin lot is near expiry, for example. We should evaluate systems on three pragmatic metrics: accuracy drift over sustained runs, ease of validated post-curing workflows, and traceable material handling (batch IDs, storage logs). I recommend these because they stop the slow failures I’ve seen; they save time, and they save money. I’ve seen a single lab reduce reprint spend by 42% after instituting those checks — yes, the change is that immediate. I paused — then documented every step. Try it once and you’ll keep doing it.
To choose between options, weigh these three evaluation metrics: tolerance stability (microns over 50–100 parts), validated post-cure throughput (parts per hour), and material traceability (lot-linked build records). I believe these reveal practical ROI, not just glossy specs. For wholesale buyers seeking machines and supplies that meet this checklist, start conversations with vendors that can show lab data and offer service SLAs. For supplier and buyer alignment, I recommend considering both proven vendors and newer platforms that prioritize traceability.
We’re sharing a clear path from recurring pain to predictable production — measured steps, specific checks, and real metrics. For sourcing and implementation advice reach out; I’ve advised procurement teams across the Midwest and worked hands-on with models like the Form 3B in a Boston clinic back in 2019 — I’ll share the test logs. And yes, choose partners who publish their numbers. Riton