



Introduction — a simple question that starts a bigger plan
Have you ever wondered why a small shop with good people still misses deadlines? I ask this because I’ve seen the same scene play out: a job lands, the team rallies, and the machine sits idle longer than it should. For CNC lathe manufacturers, that gap between potential and output is the design problem we keep circling (and yes — it shows up in the invoices).
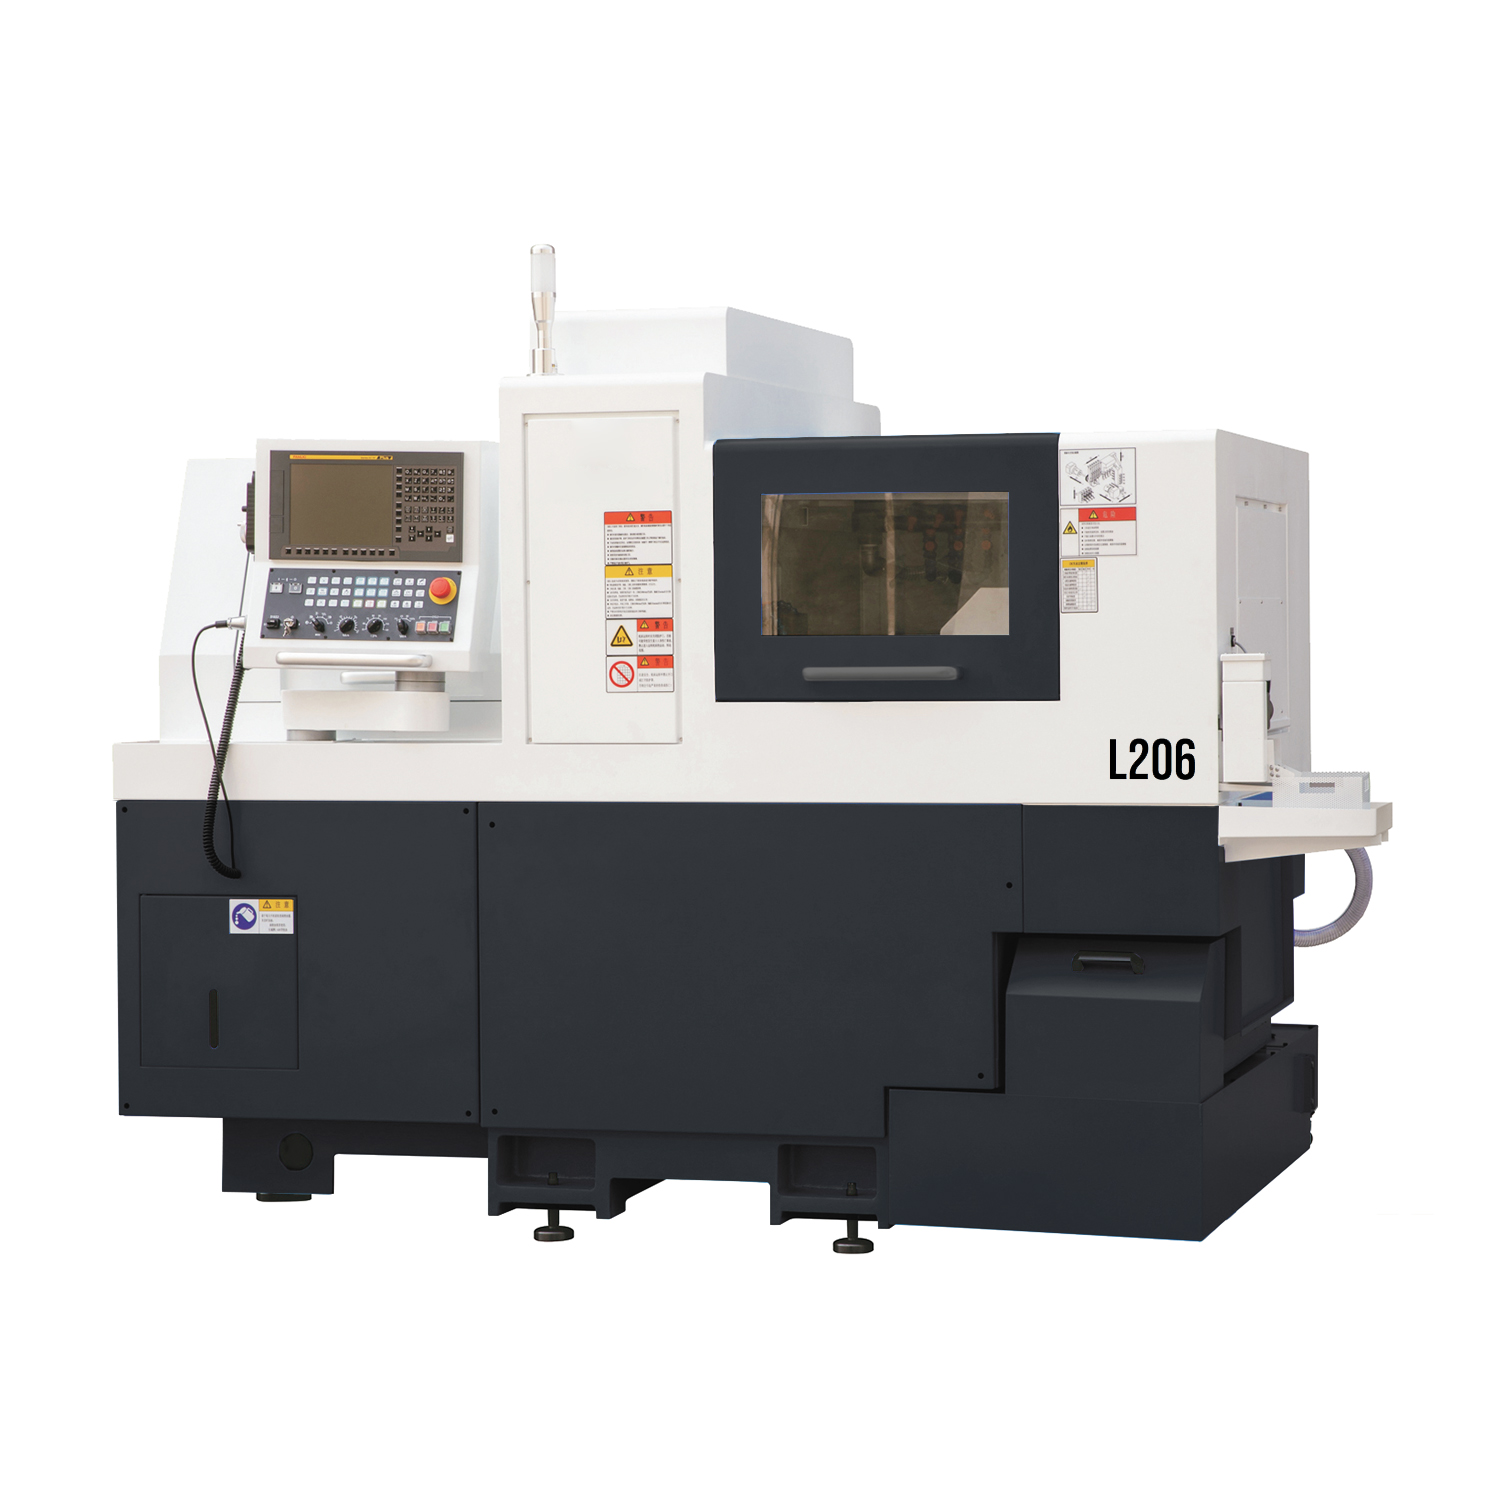
Here’s the quick data point that makes this matter: shops report up to 30% lost production time when setups and tool changes are clumsy. As a cloud architect might frame it, you need scalable throughput, predictable latency, and modular control — but for metal, not packets. So what single change moves the needle for both speed and quality? Let’s map the problem and then look at why many fixes fall short. Next, I’ll dig into where the usual fixes break down and what users quietly tolerate.
Part 2 — Where traditional fixes fail (technical look)
When I talk to machinists and engineers, they point to the same weak spots: slow tool change, poor integration, and unreliable feedback loops. The deeper issue is that many shops still rely on bolt-on solutions that treat the machine like a box rather than a system. I want to call out one central element: the live tool capability. If you are shopping, check a live tool cnc lathe early (I mean it) because it changes setup time, part geometry options, and cycle planning in one move.
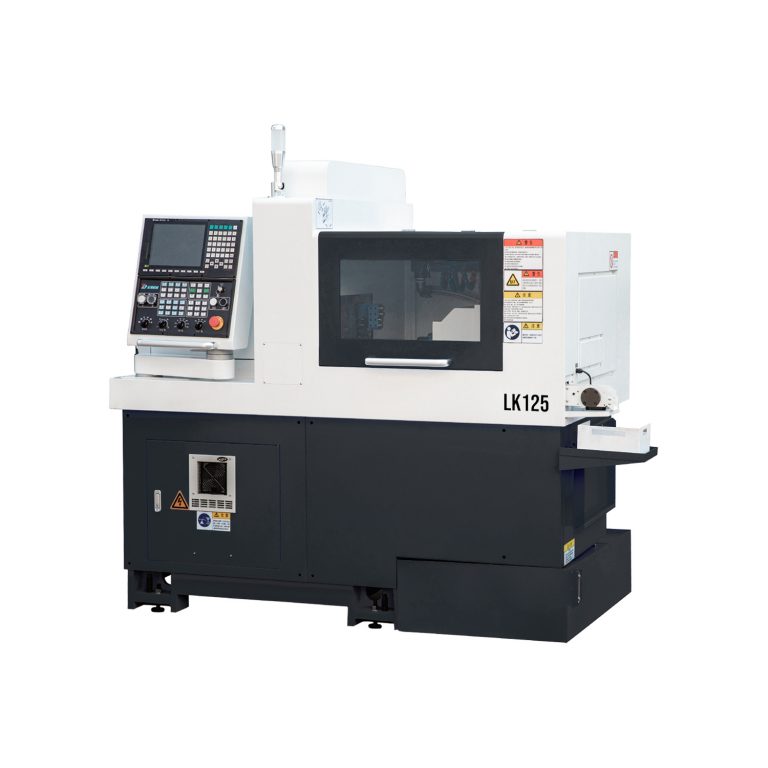
How exactly does this break things?
First, tool turret swaps cost minutes and waste tolerance. Second, spindle speed control and power converters tuned for old cycles don’t handle mixed runs well. Third, control systems often lack edge computing nodes to process sensor data close to the machine, so latency kills predictive maintenance. I’ve seen setups where operators hand off parts between machines because the lathe couldn’t pivot fast enough. Look, it’s simpler than you think: removing friction at the tool interface and closing the sensor loop reduces downtime more than any marketing spec sheet will tell you.
We also have to admit user pain that rarely gets named. Operators accept band-aid fixes — manual offsets, repeated test cuts, sticky notes with settings. These are invisible costs. They add up to scrap, rework, and stress. As someone who’s watched plants iterate through fixes, I find that the best gains come from rethinking the control and tooling architecture together, not from upgrading one component in isolation—funny how that works, right? The next section will compare emerging approaches and give a practical lens for choice.
Part 3 — Future outlook: real examples and how to choose
What’s next? I like to look at two paths: modular retrofit and integrated new builds. In one shop I visited, the owner chose a new live tooling package with higher torque motors, tighter spindle speed control, and a smarter tool turret. They cut setup time by half and lowered scrap rates. In contrast, a nearby shop added sensors but left the old turret; results were mixed. My point: hardware and control need to evolve together. If you read reviews from top cnc lathe companies, you’ll see this pattern — integration beats addition more often than not.
Real-world impact — what to watch for
So when you evaluate options, I recommend a short checklist that I use with teams. First, measure true cycle time including set up and changeovers. Second, demand closed-loop feedback — not just alarms but actionable data. Third, ask how the system will scale: can it take on mixed parts without constant tuning? These are simple questions. They keep conversations practical and make ROI clear. Yes, really.
To close with three concrete metrics you can use right away: 1) Average setup time per job (minutes), 2) Mean time between unplanned stops (hours), 3) Percentage of parts needing rework (%). Weigh these when you compare tool turrets, spindle specs, or control platforms. I’ve worked with shops that thought specs alone told the story. They were wrong. Integration, operator flow, and predictable maintenance matter more.
In short, I believe the best choices come from testing integrated solutions on real jobs, not from trusting glossy brochures. If you want to start small, test one cell with a live tooling setup and measure those three metrics. You’ll learn fast — and you’ll see where to invest next. For more practical gear and options, check Leichman.
